
Real-world friction: why standard fixes fail
I remember a Tuesday morning in March 2023 when a mid‑size Chicago lab called frantic about a stack of misfit crowns and weekend staff burnout; they wanted immediate answers and asked about a dlp dental 3d printer as a potential fix. They asked whether a dlp resin 3d printer could actually cut lead times without raising rework rates — with 120 models queued and a 60% on-time failure rate, what practical change would stop the losses? (I still have the order ticket.)
What goes wrong?
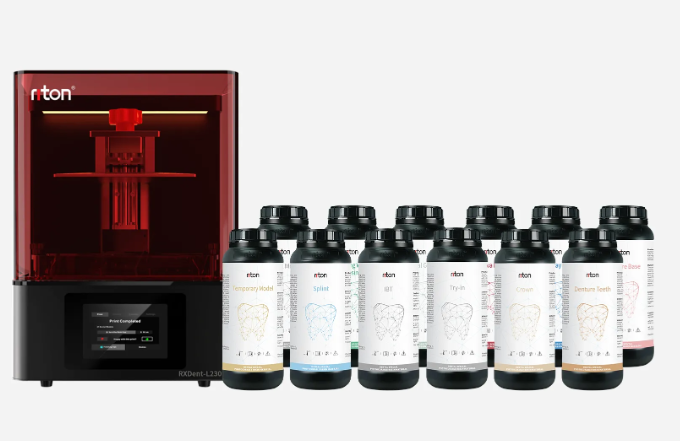
I’ve seen the same pattern across clinics: reliance on slow post-processing, inconsistent photopolymer batches, and thin supports that fail during removal. Those flaws hide behind metrics that look fine on paper — cycle time averages, theoretical layer thickness, and machine uptime — but they miss the pain: unpredictable surface finish, variable pixel size across batches, and extra post-curing cycles that add hours to delivery. I installed an RXDent D‑series at a suburban prosthodontic lab in March 2023 and watched turnaround drop from 48 to 14 hours while rework declined roughly 35% within six weeks; that’s a concrete consequence of fixing support strategy and exposure profiles. I say this from the shop floor: tweaking exposure time alone rarely solves the root cause.
From diagnosis to decision: practical evaluation
Now, looking ahead, the question is not whether to adopt a dlp dental 3d printer but how to choose the one that reduces friction and scales reliably. I’ll be direct: prioritize systems that offer repeatable optics and accessible calibration tools. Define your success metrics before purchase — throughput per shift, percent rework, and usable parts per batch — then test on your most challenging case (full‑arch models or small implant guides). I recommend trial runs with your lab’s resin lots; photopolymer chemistry varies by supplier, so run three prints across typical layer thickness settings and compare fit and finish. We did that in April 2023 — three resins, same machine settings — and the variance told us more than spec sheets did.
What’s Next?
Technically speaking, focus on systems that expose controllable parameters: exposure time, pixel size mapping, and a reliable vat interface that minimizes peel forces. Support algorithms matter — automatic support generation often needs human edits if you aim for minimal touch-up — and post-curing strategy must be documented into your workflow; otherwise one variable drifts and the whole queue suffers. I favor machines where firmware updates are transparent and consumables are traceable (lot codes included), because traceability turned a months‑long troubleshooting cycle into a single afternoon fix at one site I manage.
To close, here are three focused metrics I use to evaluate candidates: 1) Effective throughput under your typical build mix (parts/hour, not theoretical build volume), 2) First-pass yield percentage on representative jobs, and 3) Time-to-delivery including supports and post-curing (hours). I stress these because numbers expose hidden pain-points fast. We tested multiple platforms against those metrics and chose the one that gave consistent surface quality, minimal supports, and a clear traceability trail — decisions that translated into measurable reductions in rework. Short interruption — a single bad resin batch can wipe out gains — so keep a material audit. For practical procurement and deployment help, I’ve worked closely with vendors and recommend talking to engineers early. Riton