
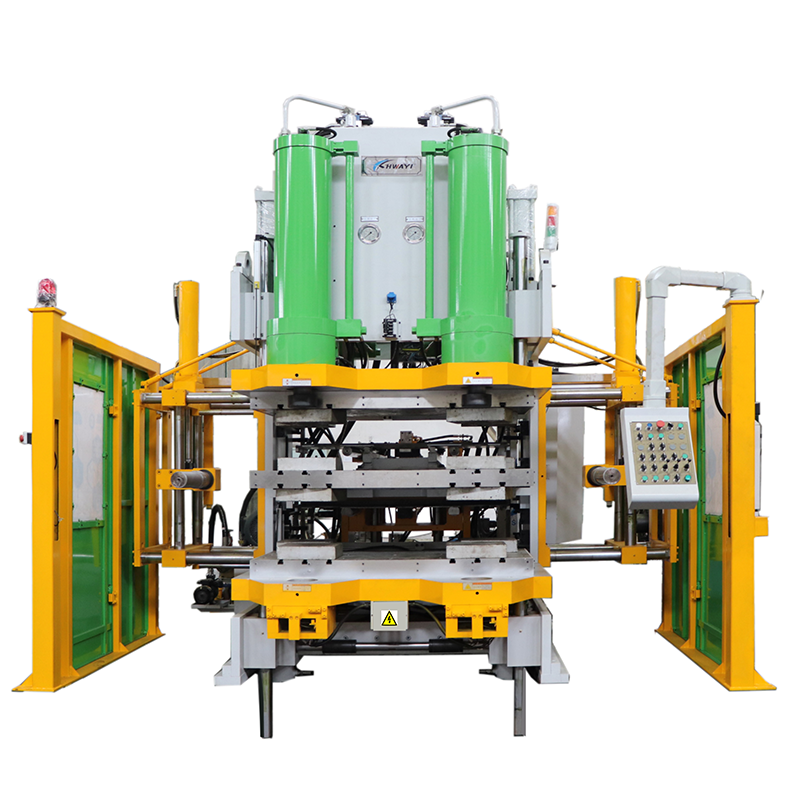
Opening comparison and context
When two presses sit side by side, one will often deliver tighter gauge uniformity than the other — not because of better material, but because its platen parallelism holds under load. This piece compares machine types, service regimes and supplier choices to show how small deviations in platen alignment ripple through an Lsr molding line. Alongside the usual items like cure cycle timing and temperature control, consider ancillary kit such as a belt vulcanizing machine rubber belt vulcanizing machine when planning throughput and downtime; peripheral reliability matters to the steady-state you want.
How platen parallelism maps to gauge uniformity
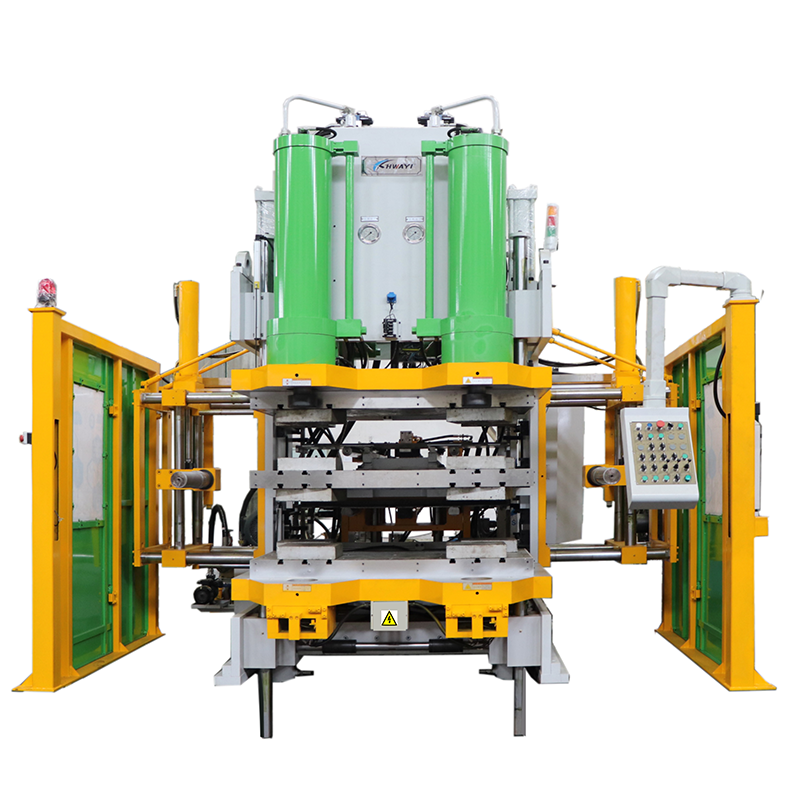
Platen parallelism is the geometric baseline: if the platens tilt even a few hundredths of a millimetre across the face, pressure distribution changes and cure thickness varies. In Lsr molding, that affects final gauge across the sheet or part. The interaction is mechanical and thermal — press pressure concentrates where the gap is smallest, heat transfer shifts, and the cure cycle no longer produces uniform cross-linking. The result is local thin spots, flash or inconsistent shore readings, not ideal for tight-tolerance runs.
Comparative view: hydraulic, mechanical and servo presses
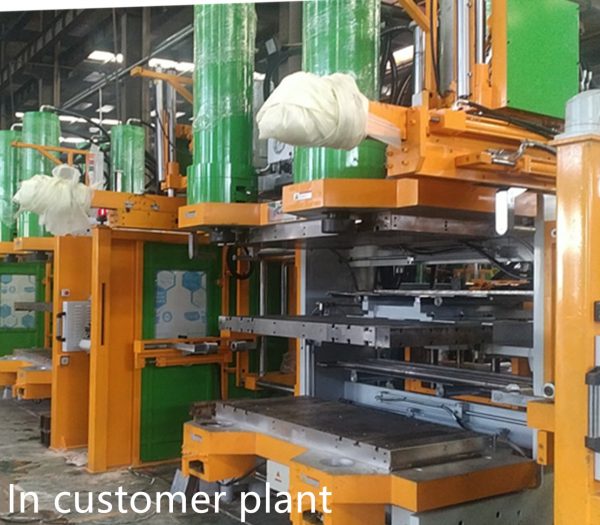
Hydraulic presses give brute steady pressure but rely on a sound hydraulic system and correct alignment checks. Mechanical presses can be fast, but any wear in toggle joints shows up as misalignment. Servo-driven presses let you monitor and correct platen motion with finer control, reducing parallelism drift during the cycle. From a sourcing angle, buyers often scout suppliers in Guangdong and other Chinese hubs where many china rubber belt track vulcanizing press manufacturers operate; choose vendors with clear calibration protocols and ISO 9001 documentation if you want predictable tolerance management.
Production fallout: measurable and repeatable losses
In practice the consequences are concrete. Scrap rates climb; inspection time rises; cycle speeds may have to be reduced to chase consistency. Gauge non-uniformity forces rework or rejects and creates variation in downstream assembly. Track these as simple KPIs: percentage of parts within tolerance, average rework minutes per shift and thermal variance across the platen. Those numbers tell you whether corrective maintenance matters more than process tweaks.
Common mistakes and practical fixes
Operators and engineers trip up by treating parallelism as a once-off set-and-forget. Regularly check with feeler gauges or dial indicators, and log readings. Use shims or retorque sequences only as interim fixes — true remedy is regrind or precision shimming and, where budgets allow, upgrading to a servo system with feedback for platen position. Calibrate thermocouples and ensure heater circuits are balanced. Predictive maintenance helps: vibration monitoring and oil analysis for hydraulic presses will flag issues well before gauge uniformity collapses — small wins that add up.
Comparing supplier value: what to insist on
When comparing vendors, pay attention to these pragmatic points. One: documented flatness and parallelism tolerances at both cold and operating temperature. Two: evidence of process controls for cure cycle repeatability. Three: spare parts availability and service response in your region — South African buyers often prefer suppliers who understand local uptime needs. Guangdong remains a production centre; recent supply-chain disruptions showed us that lead times and service infrastructure matter as much as price. — It’s a lesson learned the hard way by many firms.
Three golden rules for selecting machines and partners
1. Measure meaningful tolerances: require vendor specs for platen parallelism under load and at operating temperature, not just cold-flat numbers. 2. Insist on closed-loop control: servo drives or pressure-feedback systems reduce drift and protect gauge uniformity during the cure cycle. 3. Verify local support: ask for service case studies or references in your region, and confirm spare-parts lead time.
HWAYI ties these threads together with machines and support that focus on consistent platen performance — the practical backbone for dependable gauge control. Final word: pick the system that keeps your tolerances honest. —