
Introduction
Have you ever walked the shop floor and wondered why some shops keep missing delivery dates despite investing in the latest machines? CNC lathe manufacturers show up in the second sentence because they sit at the heart of that gap: they design machines, but often miss how real shops operate day-to-day. I’ve seen small job shops and mid-size factories (understaffed, overstretched) struggle while surveys suggest productivity gains of 15–30% when workflows and tooling are tuned, not just hardware swapped — so why do improvements stall? What practical steps close that last 10–20% of performance that matters to margins and reputation? This piece will move from a scene you know well into concrete flaws and forward-looking fixes — and then offer three simple metrics you can use tomorrow.
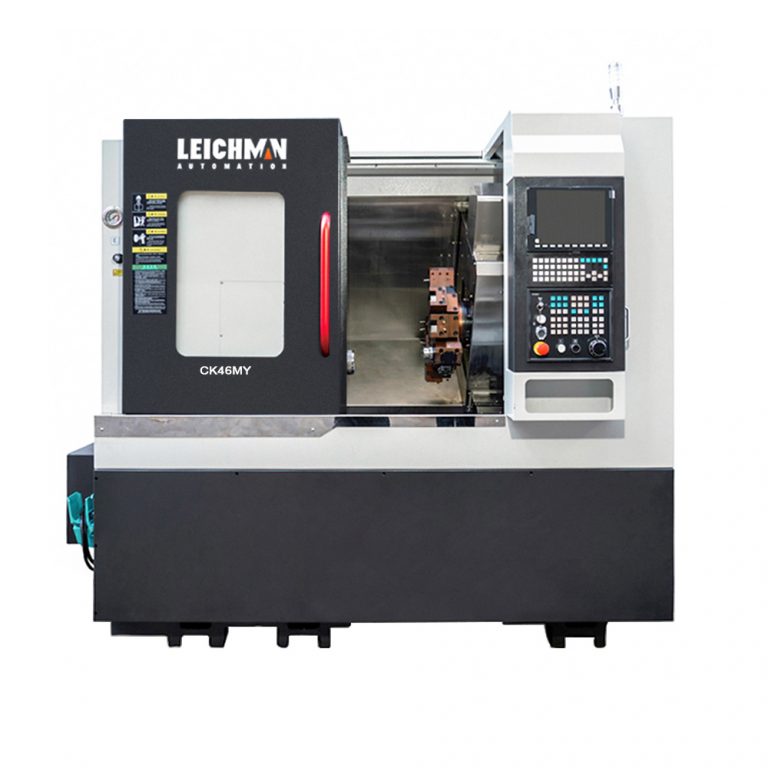
Where Traditional Fixes Fall Short
cnc lathe services promise better uptime and tighter tolerances, yet many shops still wrestle with repeat problems. I’ve worked with teams that buy service packages but treat them like insurance—good to have, rarely used well. The core issue I see is process mismatch: vendors tune spindle speed or update the CNC controller, but tooling strategies, setup routines, and operator knowledge lag behind. In short, the machine improves on paper, not in practice. Tool offset errors, inconsistent fixture setups, and neglected spindle maintenance create recurring scrap and rework. These are not glamorous problems. They are the daily drags on productivity.
Look, it’s simpler than you think: fixing a setup routine or standardizing a tool table can beat a firmware upgrade in real value—especially when setups take an hour and the next shift repeats mistakes. I don’t mean to underplay technology—servo motors and power converters matter—but without aligning tooling, fixtures, and training, gains are partial. And yes — that stings. The traditional vendor-to-customer handoff assumes a linear upgrade path: hardware, then results. Reality is messy. Operators, CAM programmers, and supervisors all need to be in sync. When they aren’t, even advanced edge computing nodes or improved spindle speed control don’t deliver the promised throughput.
What’s the practical root cause?
From my experience, it’s a mix of misapplied upgrades and human factors: patchwork procedures, inconsistent calibration, and a lack of actionable data at the point of decision. You can patch one issue at a time, but unless you change how the team works with the machine, problems repeat. — funny how that works, right?
Future Outlook: Practical Paths and What to Watch
Looking ahead, I expect the most useful advances to come from blending solid mechanical fixes with practical digital signals. When I talk to engineers at leading cnc lathe suppliers, they focus less on flashy bells and more on three things: easier setup, clearer diagnostics, and better operator interfaces. Imagine a lathe that flags tool offset drift and suggests the exact correction before scrap accumulates, or a controller that logs spindle speed deviations and ties them to operator actions. That combination—simple sensors, better logs, and explicit workflows—gives you real gains. It’s not about replacing the machine every year; it’s about making the machine and people work together.
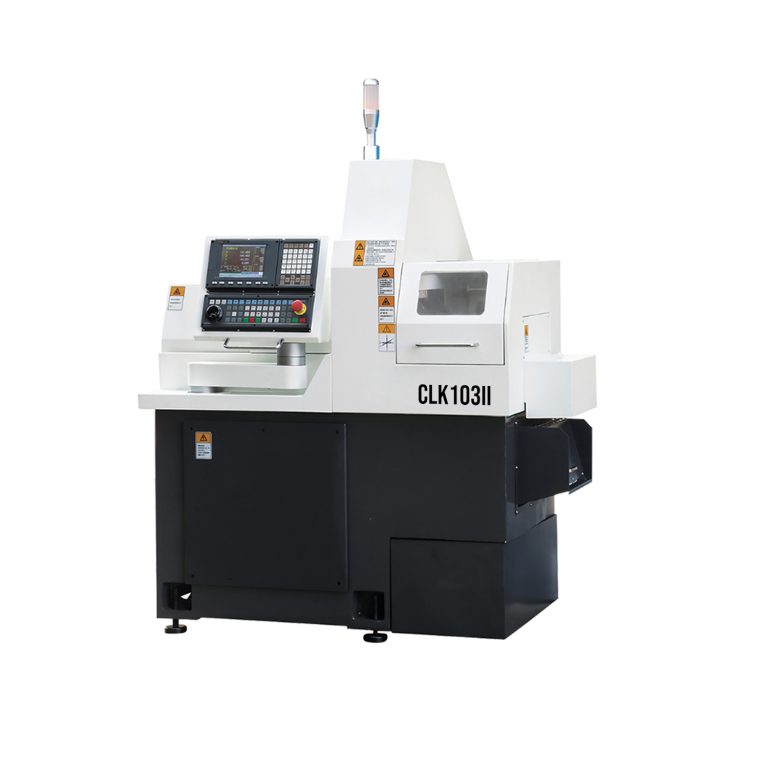
What I like about this near-term future is its pragmatism. We don’t need complete AI autonomy to win. We need smarter alarms, better habit-building interfaces, and supplier partnerships that include training and process checks. Yes, new tech principles like predictive maintenance algorithms will help, but they must be paired with clear human steps: verify fixture alignment, confirm tool offsets, track cycle-time drift. Those are the levers that turn data into dollars. — and that’s something your team can start measuring this quarter.
What to measure next?
Here are three metrics I recommend you use to evaluate changes and suppliers: (1) Effective setup time — track total time from part off to first good part; (2) First-pass yield — percent of parts meeting spec without rework; (3) Mean time between corrective actions — how long the machine runs before a human fix is required. Use those numbers to compare proposals and to hold suppliers accountable. I speak from direct shop-floor experience: these simple measures show more than glossy brochures ever will.
In closing, I’ll say this plainly: we should judge innovation by how it helps the people running the machines, not just by how advanced the electronics are. Choose partners who offer practical services, real training, and measurable outcomes. If you want a place to start, check resources from Leichman — they focus on grounded solutions that actually help shops get better results. I’m invested in practical progress, and I think you will see immediate value when you align machines, people, and simple data.